chemical supplier in UAE

Why OOZECHEM is best Chemical Supplier in UAE and GCC?

Finding the best chemical supplier in UAE is important for industries that depend on consistent quality, reliable supply, and suitable chemical solutions. From manufacturing and water treatment to oil and gas, construction, pharmaceuticals, and food processing, businesses require dependable access to industrial and specialty chemicals.

OozeChem supplies a wide range of industrial and specialty chemicals in the UAE, supporting businesses with quality products, reliable supply, and regional distribution. This guide explores the key factors to consider when choosing a chemical supplier and the chemical solutions available for different industrial appl

What Makes a Chemical Supplier “The Best” in the UAE?

A leading chemical supplier must provide more than just products. The most trusted chemical companies in the UAE are defined by:

  • Proven chemical performance and consistency
  • Understanding of industrial applications
  • Compliance with regional and international standards
  • Reliable logistics across the GCC
  • Ability to support multiple industries

OOzechem meets all these criteria, which is why it is trusted across the Middle East.

Core Chemical Solutions Offered by OOzechem

Desiccant Silica Gel

Moisture control is essential in industries such as pharmaceuticals, electronics, logistics, and packaging. OOzechem supplies high quality Desiccant Silica Gel designed to effectively absorb moisture and protect products from humidity related damage.

Silica gel from OOzechem is known for:

  • High adsorption capacity
  • Stable performance in varied climates
  • Long service life

This makes it ideal for UAE’s high humidity environments and long distance shipping needs.

Caustic Soda Flakes

Caustic Soda Flakes in KSA are a fundamental industrial chemical used in manufacturing, textiles, soap production, water treatment, and chemical processing.

OOzechem supplies caustic soda flakes that offer:

  • Consistent alkalinity
  • High purity for industrial reactions
  • Reliable solubility and performance

This reliability is critical for industries that depend on precise chemical reactions and controlled processes.

Molecular Sieve

In gas drying, air separation, and purification systems, performance depends heavily on adsorption efficiency. Molecular Sieves supplied by OOzechem are engineered for precise separation of molecules based on size.

These products are widely used in:

  • Oil & gas processing
  • Industrial gas production
  • Refrigeration and drying systems

OOzechem’s molecular sieves support operational efficiency and equipment longevity.

Calcium Hypochlorite

Water sanitation and disinfection are critical in the UAE’s municipal and industrial sectors. Calcium Hypochlorite in UAE supplied by OOzechem is a powerful disinfectant used in water treatment, swimming pools, and sanitation systems.

Key benefits include:

  • Strong chlorine content
  • Effective microbial control
  • Stable shelf life

This makes it a dependable solution for both public and private water treatment operations.

Carbon Molecular Sieve

For industries using nitrogen generators, Carbon Molecular Sieve is an essential material. OOzechem supplies carbon molecular sieves that enable efficient nitrogen separation from air.

These products are commonly used in:

  • Industrial nitrogen generation
  • Food packaging
  • Electronics and metal processing

Their durability and performance consistency make them suitable for continuous industrial use.

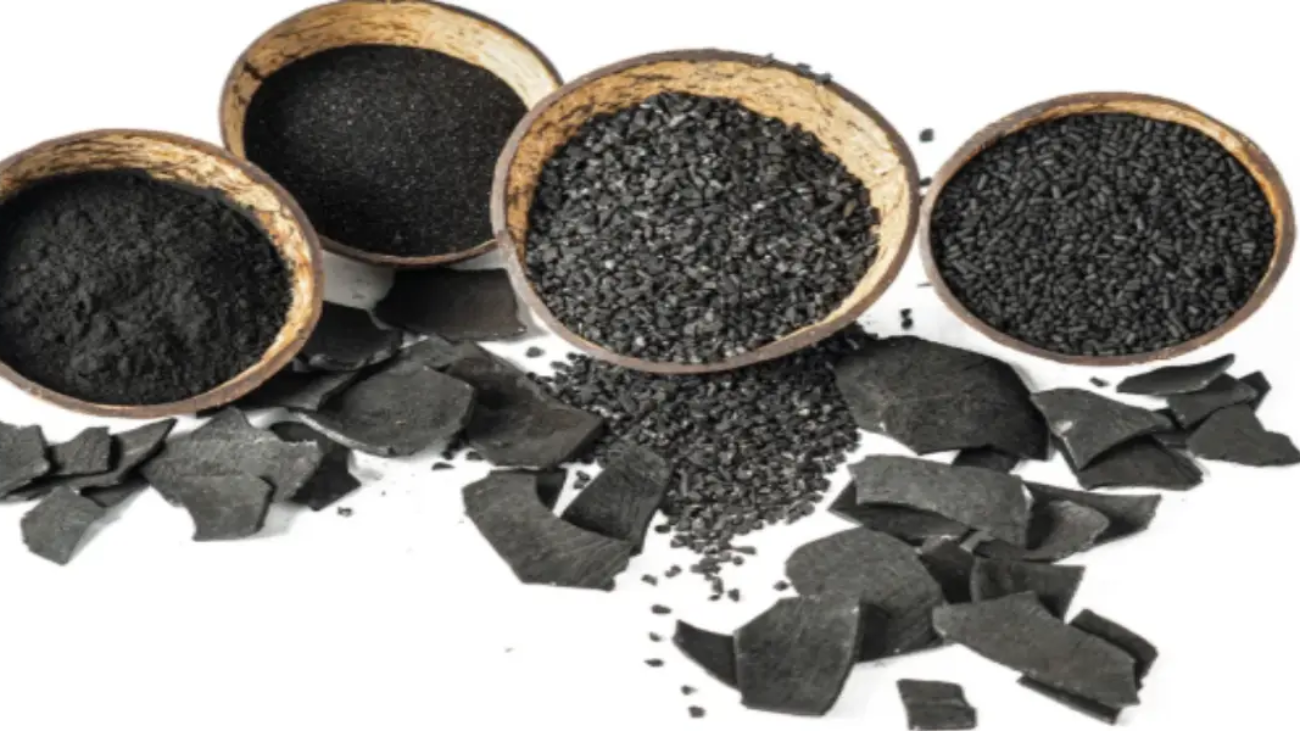
Activated Carbon

Purification and filtration processes rely on adsorption efficiency. Activated Carbon supplied by OOzechem is used extensively for removing impurities, odors, and contaminants from air and water.

Activated carbon plays a vital role in:

  • Water treatment plants
  • Air purification systems
  • Industrial effluent treatment

OOzechem’s activated carbon solutions support environmental compliance and clean processing.

Sodium Benzoate

Sodium Benzoate is widely used as a preservative in food, beverage, and pharmaceutical industries.

OOzechem supplies sodium benzoate that offers:

  • Consistent chemical stability
  • Compliance with industrial usage requirements
  • Reliable performance in formulations

This makes it a trusted ingredient for manufacturers across the GCC.

Activated Alumina

Drying and purification processes often require advanced adsorption materials. Activated Alumina supplied by OOzechem is used for moisture removal, fluoride removal, and air drying.

It is commonly applied in:

  • Water treatment systems
  • Compressed air drying
  • Industrial purification units

Its high surface area and mechanical strength ensure long-term efficiency.

Regional Supply Across UAE & GCC

OOzechem’s strong logistics network allows it to serve customers across:

  • United Arab Emirates
  • Qatar
  • Oman
  • Saudi Arabia (KSA)
  • Kuwait

This regional presence ensures fast delivery, consistent availability, and dependable support for cross border industrial projects.

Why Industries Trust OOzechem?

Industries choose OOzechem because it offers:

  • Technical understanding of chemical applications
  • Stable product quality across batches
  • Long term supply reliability
  • Multi-industry chemical expertise

Rather than acting as a simple trader, OOzechem operates as a chemical solutions partner.

Conclusion

OOzechem’s position as the best chemical supplier in UAE is built on quality assurance, industrial knowledge, reliable logistics, and customer trust. Its ability to support industries across the UAE, Qatar, Oman, KSA, and Kuwait makes it one of the most dependable chemical suppliers in the GCC.

For businesses seeking consistent performance and professional chemical supply, OOzechem stands out as a trusted industry leader in the Middle East.
Also Check :

Best Adsorbents in UAE

Best Adsorbents in Gulf Countries

Industrial operations in the Gulf region face a unique challenge: extreme heat, high humidity, and continuous exposure to moisture laden air. These harsh environmental conditions make the selection of the right adsorbent critical for industries such as oil & gas, petrochemicals, water treatment, pharmaceuticals, food processing, and packaging.

In this guide, we explore the best adsorbents for Gulf climate, how they work, the difference between absorbent and adsorbent, and why certain materials like activated carbon, silica gel, and molecular sieves outperform others in hot and humid regions like the UAE, Saudi Arabia, Kuwait, Qatar, Oman, and Bahrain.

What Is an Adsorbent?

An adsorbent is a solid material that attracts and holds molecules, gases, or moisture on its surface. Adsorbents are widely used in gas purification, moisture control, solvent recovery, industrial drying, and environmental applications.

Many people confuse absorbent and adsorbent, but the difference is simple:

  • Absorbent: absorbs substances into its internal structure (like a sponge).
  • Adsorbent: attracts substances onto its surface.

Industrial processes in the Gulf rely heavily on adsorbents because they efficiently remove moisture, impurities, and contaminants, even in extreme climatic conditions.

Top Types of Adsorbent in UAE & Gulf Industries

Below are the four most effective adsorbents for Gulf conditions and how they perform.

1. Molecular Sieve Adsorbent

A molecular sieve adsorbent is a crystalline aluminosilicate with uniform micropores that trap moisture and gases selectively. Grades like 3A, 4A, 5A, and 13X are widely used in the region.

Why They Work Best in Gulf Climate

  • High adsorption capacity even at extreme temperatures
  • Highly stable structure
  • Can reduce moisture to PPM levels
  • Suitable for PSA oxygen & nitrogen generation

Industries Using Molecular Sieves in GCC

  • Petrochemicals
  • Gas drying (natural gas & LPG)
  • Oxygen & nitrogen generators
  • Ethanol dehydration
  • Refrigerants
  • Air separation units

2. Silica Gel Adsorbent

A silica gel adsorbent is ideal for moisture control in storage and logistics especially across humid Gulf ports such as Jebel Ali, Bahrain, Muscat, and Dammam.

Advantages in Gulf Climate

  • Excellent moisture control for consumer & industrial goods
  • Works effectively in 70–90% humidity
  • Non-toxic and cost effective

Best Uses

  • Container desiccants
  • Electronics packaging
  • Pharmaceuticals
  • Food grade moisture control

Explore more about Desiccants!

3. Activated Carbon Adsorber System 

Activated carbon adsorbers are essential for the removal of VOCs, odors, gases, and organic compounds. They “adsorb by activated charcoal”, making them perfect for high pollution zones.

Why Activated Carbon Works in GCC

  • Massive surface area for adsorption
  • Removes industrial fumes in petrochemical zones
  • Effective in high heat
  • Works with humid Gulf air

Common Applications

  • Air purification
  • Water treatment plants
  • Oil & gas refining

Industrial chimneys & scrubbers

 Carbon Molecular Sieve (CMS)

CMS is essential for PSA nitrogen generators, especially in Gulf industries where reliable nitrogen supply is critical.

Why CMS Works in Gulf Climate

  • Stable at high temperatures
  • Precise gas separation
  • High N2 purity

Explore More About PSA nitrogen systems

How to Choose the Best Adsorbent for Gulf Conditions?

Temperature Tolerance

The Gulf’s extreme heat demands an adsorbent that performs well above 45°C. Molecular sieves maintain strong adsorption capacity in UAE & Saudi environments, making them ideal for high temperature industrial processes.

Humidity Handling

Coastal areas like Dubai, Abu Dhabi, Sharjah, Dammam, and Doha face very high humidity. In these conditions, silica gel & activated carbon work best because they continue adsorbing moisture and VOCs even when the air is saturated.

Purity Requirements

Industries needing PPM-level drying such as gas production, pharma, and food processing should choose molecular sieves, which provide the highest purity and most precise moisture removal.

Regeneration Capability

For continuous Gulf operations, select adsorbents that can be regenerated using heat, vacuum, or pressure swing (PSA systems). This reduces downtime and improves long term efficiency.

Availability & Supplier Reliability

Since the Gulf heavily relies on imports, always source adsorbents from a trusted supplier in UAE to ensure consistent stock, fast delivery, and reliable support.

Applications of Adsorbents in UAE 

IndustryApplications
Oil & GasGas drying, VOC removal, Refinery purification
Desalination PlantsMoisture control, Odor removal
Pharmaceutical & Food IndustriesPackaging moisture control,  Purity protection
Manufacturing PlantsCompressed air drying, PSA oxygen/nitrogen generation
Shipping & LogisticsContainer desiccants, Warehouse moisture protection

Which Adsorbent Is the Best for Gulf Climate?

ApplicationBest Adsorbent
Moisture drying to PPMMolecular Sieve
Warehouse & packagingSilica Gel
VOC & gas removalActivated Carbon
PSA nitrogen systemsCarbon Molecular Sieve
Air purificationActivated Carbon
Chemical refining13X Molecular Sieve

Each material has its strengths, but combined systems (silica gel + activated carbon or molecular sieve + CMS) offer maximum protection.

Best Adsorbent Suppliers in UAE and Gulf

OozeChem stands out as one of the best adsorbent suppliers in UAE and Gulf, offering:

OozeChem’s products are engineered for extreme Gulf temperatures, ensuring high adsorption capacity, durability, and performance.

Conclusion

The Gulf region’s extreme heat and humidity make the choice of the right adsorbent crucial for industrial efficiency, safety, and product quality. Whether you need molecular sieve adsorbent for gas drying, silica gel adsorbent for storage protection, or carbon adsorbers for air purification, selecting the right material ensures your operation remains stable year round.

If you’re looking for high performance adsorbents in UAE and Gulf, OozeChem provides reliable, industry tested solutions. Contact us Today! 

Take a Look at Activated Alumina vs Silica Gel blog

Caustic Soda Types

Grades and Types of Caustic Soda

Looking for the right caustic soda flakes for your business in the Gulf? Whether you run a detergent factory, a water treatment plant, or a cleaning supplies company, understanding the grades and types of caustic soda can save you time, money, and a lot of confusion.

At OozeChem, your trusted caustic soda flakes supplier in UAE and across all Gulf countries, we’re here to make this chemical crystal clear (pun intended!). Let’s dive into everything you need to know  from the caustic soda formula to the best applications and how to choose the right grade for your needs.

What Is Caustic Soda?

Caustic soda, also known as sodium hydroxide, is a powerful alkali used in nearly every industry from soap manufacturing to water purification. Its chemical formula is NaOH, which stands for sodium (Na), oxygen (O), and hydrogen (H). In simple terms, that’s what caustic soda is made of. This highly versatile compound comes in several forms, including caustic soda flakes, caustic soda pearls, and caustic soda liquid, each offering distinct advantages depending on your application and industry needs.

Types: Flakes, Pearls, and Liquid

Think of these types as the same ingredient  just in different “packaging.”

Caustic Soda Flakes

These are white, brittle flakes of sodium hydroxide. They’re easy to store, dissolve, and transport.
Best for: Soap making, cleaning products, textiles, and water treatment.
Fun fact: Most industries in the UAE and Saudi Arabia prefer flakes for their long shelf life and ease of handling in dry Gulf climates.

Caustic Soda Pearls

Tiny, round beads that look a bit like small white pearls.
Best for: Automated systems and industries that require precise dosing.
Why choose pearls? They create less dust and dissolve faster than flakes.

Caustic Soda Liquid

A ready-to-use liquid form (usually 50% NaOH).
Best for: Large-scale or continuous operations like wastewater treatment or chemical manufacturing.

Comparison of forms

FormTypical Use CasesAdvantages
FlakesIndustrial batch processes, soap & detergent lines, textile scouringEasy to store and measure, longer shelf life
Pearls (prills)Automated feeding systems, water treatment dosing, where dust control is keyLow dust, rapid dissolution
Liquid solutionContinuous feed processes, wastewater treatment, where the dissolution step has already been doneReady-to-use, eliminates solid dissolution ste

Grades of Caustic Soda

Grades define how pure your caustic soda is, while types define its physical form. So, you can have technical-grade flakes or food-grade flakes.

Let’s look at the most common grades used in the Gulf region:

GradePurity LevelTypical Use
Technical Grade96–98%Ideal for industrial use (pH control, soap, textiles, etc.)
Industrial Grade98–99%Suitable for large manufacturing and chemical processes
Food Grade≥99%Used for food processing and cleaning in food industries
Reagent/Pharma Grade≥99.5%Used in laboratories and pharmaceuticals

At OozeChem, we supply caustic soda flakes in multiple grades  ensuring you get the right purity for your exact application.

Caustic Soda Applications

 Soap & Detergent Manufacturing

This is one of the biggest uses in the Gulf!
NaOH reacts with fats and oils to produce soap. It’s also used to create detergents and degreasers.

Textiles & Dyeing

Textile factories use caustic soda for mercerizing cotton, a process that gives fabrics more shine and strength.

Water Treatment

Caustic soda neutralizes acids and adjusts the pH of water  making it safe and stable for industrial use.

Paper & Pulp

Used to separate cellulose fibers during paper production.

Oil & Gas Refining

In refineries, NaOH helps remove acidic impurities like hydrogen sulfide and fatty acids.

Caustic Soda for Cleaning

Because it breaks down grease, oil, and organic matter, caustic soda is used in heavy-duty cleaners and drain openers.

Choosing the Right Form for Your Business

Not sure whether you need flakes, pearls, or liquid? Here’s a quick checklist:

Go for flakes if you want:

  • Long shelf life
  • Easy transport
  • Flexibility to make your own solution

Choose pearls if you need:

  • Precise dosing in automated systems
  • Less dust during handling

Pick liquid if you prefer:

  • Ready-to-use form
  • No mixing or dissolving required

If you’re still unsure, our team at OozeChem can guide you to the best option for your process  whether you’re in Dubai, Saudi Arabia, Oman, or Qatar.

Final Thoughts

Choosing the right grade and form of caustic soda whether flakes, pearls, or liquid is key to achieving the best product quality and cost efficiency. With its simple yet powerful formula (NaOH), caustic soda is used across industries from cleaning to oil refining. That’s why partnering with a trusted regional expert matters. OozeChem, your reliable caustic soda flakes supplier in the UAE and all Gulf countries, delivers high purity, consistency, and prompt service.

OozeChem’s Product List

Oil and gas Refining

Activated Carbon for Oil and Gas Refining

Activated Carbon for Oil and Gas Refining plays an important role in purification, contaminant removal, and process treatment across the oil and gas industry. Its strong adsorption capacity makes activated carbon useful for applications such as crude oil refining, natural gas purification, hydrocarbon treatment, and wastewater treatment, helping industries maintain cleaner and more efficient processes.

OozeChem supplies high-quality activated carbon for oil and gas applications in the UAE and across Gulf markets. In this guide, we explore how activated carbon works, its key applications in oil and gas refining, and the factors to consider when selecting the right activated carbon for indus

What Is Activated Carbon?

Activated carbon is a specially processed form of carbon known for its extensive porous structure and massive internal surface area. This unique structure allows it to adsorb impurities and contaminants from gases and liquids, making it indispensable in industrial purification.

How activated carbon works is quite fascinating: impurities are trapped in its pores via adsorption a process where molecules adhere to the surface without chemical reaction, efficiently removing unwanted compounds. This is why activated carbon filters are common in many industrial and environmental applications.

Activated Carbon Adsorption: The Science Behind the Magic

The activated carbon adsorption process is all about surface interaction. When gas or liquid passes through an activated carbon bed or filter, pollutants stick to the carbon surface due to van der Waals forces. The high surface area, often exceeding 1000 m² per gram, means more contaminants can be trapped effectively.

This makes activated carbon filters essential in removing sulfur compounds, mercury, volatile organic compounds (VOCs), and other hazardous substances from oil and gas streams.

Activated Carbon in Oil and Gas Refining: Key Applications

1. Gas Purification and Sweetening

One of the primary uses of activated carbon in oil and gas refining is purifying natural gas and refinery gas streams. Impurities such as hydrogen sulfide (H₂S), mercaptans, and mercury must be removed to meet stringent product specifications and protect downstream equipment.

Activated carbon filters, often impregnated with sulfur or other chemicals, effectively adsorb these impurities, safeguarding catalysts and ensuring smooth operation.

2. Hydrocarbon and Liquid Stream Treatment

Activated carbon is also used extensively to decolorize and deodorize oils, lubricants, and condensates in refineries. By adsorbing trace organics and sulfur compounds, it helps improve product quality and stability.

3. Produced Water and Wastewater Treatment

Oil and gas operations generate large volumes of wastewater containing hydrocarbons, heavy metals, and organic contaminants. Activated carbon filters play a vital role in treating this produced water by adsorbing residual pollutants and reducing chemical oxygen demand (COD), helping companies meet environmental standards.

4. Vapor Recovery and Emission Control

Activated carbon filters help capture hydrocarbon vapors and VOCs released during refining and petrochemical operations. This prevents environmental pollution, recovers valuable hydrocarbons, and supports sustainability goals.

How Activated Carbon Filter Works: Understanding the Principle

The activated carbon filter working principle is based on physical adsorption. Polluted gas or liquid enters the filter and comes into contact with activated carbon. Due to the porous structure and large surface area, contaminants stick to the carbon surface, and purified fluid exits the system.

Filters can be granular (GAC), pelletized, or powdered (PAC), each suited for different industrial applications in oil and gas.

Choosing the Right Activated Carbon for Oil & Gas Refining

Selecting the perfect activated carbon product depends on:

  • Form and particle size: Granular activated carbon (GAC) is common in fixed bed systems, while powdered activated carbon (PAC) is used for rapid treatment processes.
  • Impregnation: Some activated carbons are chemically modified to target specific contaminants like mercury or H₂S.
  • Pore structure and surface area: Matching pore size distribution to contaminant size enhances adsorption efficiency.
  • Operating conditions: Temperature, pressure, and chemical compatibility matter to ensure longevity and performance.

Why Partner with OozeChem?

As the best chemical supplier in UAE and the best activated carbon supplier in UAE, OozeChem offers premium quality activated carbon tailored to the needs of the oil and gas industry. With deep technical expertise, regional distribution capabilities, and a customer focused approach, OozeChem ensures you get the right product, on time, every time.

Whether you need activated carbon for gas purification, liquid treatment, or wastewater management, OozeChem’s range covers all grades and forms. Their expert team can guide you through the selection process to maximize operational efficiency and reduce costs.

Benefits of Using Activated Carbon in Oil & Gas Refining

  • Improved product purity: Effective removal of sulfur, mercury, and organics enhances oil and gas quality.
  • Equipment protection: Adsorption of harmful contaminants protects catalysts and process equipment from damage.
  • Regulatory compliance: Helps meet environmental and safety standards for emissions and wastewater treatment.
  • Cost efficiency: Reduces maintenance, downtime, and chemical usage.
  • Environmental sustainability: Limits harmful emissions and supports cleaner water discharge.

Summary

Activated carbon is a powerful and versatile solution in oil and gas refining. Understanding how activated carbon works and selecting the right type of activated carbon filter can significantly improve process efficiency and product quality.

For companies operating in the UAE and Gulf region, partnering with a trusted supplier like OozeChem ensures access to high quality activated carbon products, expert advice, and reliable logistics.

If you want to enhance your refinery’s performance and environmental compliance, start with activated carbon and start with OozeChem.

Related Resources:

What is sodium benzoate?

What Is Sodium Benzoate?

Sodium benzoate is the sodium salt of benzoic acid and a widely used food preservative and antimicrobial agent. It helps prevent the growth of bacteria, yeast, and fungi, particularly in acidic foods and beverages, helping maintain product quality and extend shelf life.

Sodium benzoate is also used in pharmaceuticals, cosmetics, personal care products, and industrial applications. Its effectiveness, versatility, and ease of use make it a commonly selected preservative across different industries.

What Is Sodium Benzoate ?

Chemically, sodium benzoate (C7H5NaO2) is the sodium salt of benzoic acid, made by neutralizing benzoic acid with sodium hydroxide.  In the food additive industry it is often referred to by its code E211 when used in the European Union. It is an odorless, crystalline powder that is highly soluble in water, especially under acidic conditions.
The compound is recognised by the U.S. Food & Drug Administration (FDA) and other regulatory bodies as generally safe when used within prescribed limits. 

How Does Sodium Benzoate Work?

Sodium benzoate functions primarily as an antimicrobial and preservative in acidic media (typically foods and drinks with pH below ~4.5). It works by inhibiting the growth of yeast, mold and certain bacteria.
When dissolved, sodium benzoate reverts to benzoic acid under acidic conditions; benzoic acid is the active form that disrupts microbial metabolism. In acidic environments, the undissociated benzoic acid molecule penetrates microbial membranes and lowers internal pH, inhibiting growth.

Types of Sodium Benzoate

Sodium benzoate is available in two primary forms: powder and granular.

Sodium benzoate Powder:

 This is the most common form, featuring fine, free-flowing crystals that dissolve easily in water. It is ideal for use in beverages, liquid medicines, and personal care formulations where rapid dissolution and uniform mixing are required.

Sodium benzoate Granular: 

Granular sodium benzoate has a coarser texture and is preferred in applications requiring controlled dissolution, such as dry food mixes, sauces, and industrial formulations. Granules reduce dust formation during handling and are easier to store in bulk.

Both forms meet international food and pharmaceutical standards, and choosing the right form depends on the intended application and manufacturing process.

Common Applications of Sodium Benzoate in UAE

Food & Beverages

Sodium benzoate is widely used as a preservative in pickles, salad dressings, mayonnaise, margarine, jams, jellies, carbonated soft drinks, fruit juices and sauces.
Because it is most effective under acidic conditions, you will often see sodium benzoate in products with low pH. It helps maintain shelf life, preserve flavour, colour and texture, and inhibit microbial spoilage.

Pharmaceuticals & Personal Care

In pharmaceuticals, sodium benzoate serves as a preservative in liquid medications such as cough syrups, and as a tablet lubricant or excipient in capsule formulations. In personal care products, it’s used in creams, lotions, shampoos, toothpaste and mouthwash to inhibit microbial contamination and extend shelf life.

Industrial Uses

Beyond food and pharma, sodium benzoate is also used in industrial applications including corrosion inhibition in coolants, stabilisers in photo processing, and even in plastics manufacturing.

Advantages of Sodium Benzoate

  • Effective broad spectrum preservative for acidic foods, beverages and personal care.
  • Cost efficient and widely used across multiple industries.
  • Extends shelf life and helps maintain quality (colour, texture, flavour) of products.
  • Enables compliance with food safety regulations and reduces spoilage risk.
  • Consumer friendly labelling (often E211 in Europe), and well understood mechanism of action.

How to Choose a Reliable Supplier in UAE?

When sourcing sodium benzoate for manufacturing especially for the Gulf region or UAE market choosing a trustworthy supplier is critical. OozeChem, as the best chemical supplier in the UAE and Gulf countries, offers:

  • High purity sodium benzoate meeting regional regulatory specifications.
  • Full documentation: Certificates of Analysis (CoA), Material Safety Data Sheets (MSDS), regulatory compliance.
  • Supply chain and logistic support across Saudi Arabia, UAE, Qatar, Oman, Kuwait and Bahrain.
  • Technical support to help you select the correct grade and ensure safe usage and storage.
    By partnering with a reputable supplier like OozeChem, manufacturers and formulators can maintain quality, compliance and reliability.

Frequently Asked Questions 

Q1: Is sodium benzoate the same as benzoic acid?
 

No. Sodium benzoate is the sodium salt of benzoic acid benzoic acid is less soluble in water and not used directly in many formulations due to solubility limits.

Q2: Can sodium benzoate be used in baby food or infant products?
 

Use in infant foods depends on regional regulations. Always verify approvals for your target market in the Gulf region and ensure infants receive only well validated formulations.

Q3: Does sodium benzoate accumulate in the body?
 

 No. Studies indicate that sodium benzoate is metabolised (conjugated with glycine into hippurate) and excreted via urine in <24 hours under normal usage.

Q4: Should manufacturers avoid combining sodium benzoate with vitamin C?
 

Caution is advised. While regulatory levels are low and safe under normal conditions, combining sodium benzoate with ascorbic acid under heat/light may form benzene. It is best practice to evaluate formulation risk.

Summary 

Sodium benzoate is a versatile, widely used preservative and antimicrobial agent, recognised for its safety and efficacy when used within established limits. It is found in foods, beverages, pharmaceuticals, personal care and industrial products. For manufacturers and formulators in the UAE and Gulf region, working with a trusted provider like OozeChem ensures you secure quality material, regulatory compliance and supply chain reliability.
Understanding what sodium benzoate is, how it works, where it is used and how to handle it correctly empowers you to make informed decisions.

Related Pages and Internal Links

To explore more about our products and grades:

What is Activated Alumina

What is Activated Alumina?

What is Activated Alumina? Activated alumina is a highly porous, granular form of aluminium oxide (Al₂O₃) that undergoes heat treatment to develop a large surface area and strong adsorption capacity. These properties make it a versatile material for drying, purification, filtration, and catalyst support across various industrial applications.

OozeChem supplies high-quality activated alumina desiccant designed for effective moisture removal, gas drying, purification, and other industrial applications. Its high adsorption capacity, thermal stability, and long service life make activated alumina a reliable choice for demanding industrial processes.

Types of Activated Alumina

Activated Alumina is commonly available in two primary forms: Activated Alumina Beads and Activated Alumina Powder, each suited for specific industrial applications.

Activated Alumina Beads 

Activated Alumina Beads are spherical, mechanically strong granules that offer high surface area and low dust content, making them ideal for use in desiccant dryers, gas drying systems, and water treatment plants. Their uniform shape ensures even packing in adsorption towers, which minimizes pressure drop and maximizes efficiency.

Activated Alumina Powder

Activated Alumina Powder is a fine, free flowing form of alumina used where surface area and reactivity are more important than physical structure. It is commonly employed as a catalyst carrier, in ceramics manufacturing, or in chemical polishing applications.

Key Properties of Activated Alumina

Here’s a table summarising the main properties and why they matter:

PropertyDescriptionWhy it matters
High specific surface areaMany interconnected pores inside the beadsMore surface for adsorption of moisture, gases, and impurities
Selective adsorptionCan preferentially adsorb certain molecules (e.g., water, fluoride)Enables targeted purification and separation
RegenerabilityCan be restored by heating/steam purgeCost effective reuse in industrial processes
Chemical & thermal stabilityWithstands aggressive gases and high temperaturesSuitable for industrial environments
Physical strength (granular form)Mechanically robust under pressureMakes it viable in packed beds, towers and flowing systems

These properties make Activated Alumina ideal for a range of uses, which we’ll explore next.

Formation & Production of Activated Alumina

Raw material and calcination

The process begins with aluminium hydroxide, typically derived from bauxite or other alumina bearing ores. This hydroxide undergoes calcination heating to high temperatures which removes bound water molecules and transforms aluminium hydroxide into aluminium oxide (Al₂O₃)

Activation and pore generation

After calcination, the aluminium oxide is further processed in the presence of steam or activating gases under controlled conditions. This activation step develops the internal pore structure creating a large surface area and the characteristic granular form. The material is then cooled, crushed and sieved to size.

Applications of Activated Alumina

Activated Alumina finds applications in many sectors. Here are some of the most common:

Gas and air drying

It is highly effective at removing moisture from compressed air, nitrogen, oxygen, hydrogen and other gases. The high affinity for water makes it a go to adsorbent for industrial gas drying systems.

Liquid drying

In applications where liquids must be stripped of moisture (e.g., solvents, oils, chemical feed stocks), Activated Alumina is packed into columns or beds and liquids are passed through to remove water. Afterwards, the adsorbent may be regenerated.

Water purification & contaminant removal

Activated Alumina is used to remove specific contaminants from water such as fluoride, arsenic, phosphates and colour or odour causing compounds. Its adsorption capacity and chemical stability make it very suitable for this purpose.

Catalyst support / chemical processing

In petrochemical and refining industries, Activated Alumina often serves as a catalyst carrier or support in processes such as the Claus process (sulfur removal from natural gas) and other catalytic reactions.

Activated Alumina vs Other Adsorbents

It’s useful to compare Activated Alumina with other adsorbents, such as molecular sieves, to understand when it is preferred.

AdsorbentPore structureWater adsorption capacityKey advantage
Activated AluminaIrregular pore sizes, many poresHigh affinity for moistureGood general purpose adsorbent; robust and economical
Molecular sieve (e.g. zeolites)Uniform, adjustable poresVery selective adsorptionExcellent for precision separations of specific molecules  

Frequently Asked Questions (FAQs)

1. What is Activated Alumina used for?

It’s used for drying gases and liquids, removing fluoride from water, and as a catalyst support in chemical processes.

2. How does Activated Alumina remove fluoride?

It adsorbs fluoride ions onto its porous surface as water flows through, reducing fluoride content effectively.

3. Can Activated Alumina be reused?

Yes, it can be regenerated by heating, allowing for multiple uses and long term cost savings.

4. What’s the difference between Activated Alumina beads and powder?

Beads are used in filtration systems; powder is used in formulations and catalyst applications.

5. Where can I buy Activated Alumina in the UAE?

OozeChem is a trusted supplier offering high quality Activated Alumina for industrial use across the Gulf.

Also Check:

Gold recovery

CIP vs CIL: Guide to Gold Recovery Systems

Gold recovery technologies have evolved to become more efficient and cost effective, with Carbon in Pulp (CIP) and Carbon in Leach (CIL) emerging as two of the most widely used methods in modern gold processing. Both techniques rely on activated carbon to extract gold from cyanide leached ore slurries, but they differ significantly in their process design and efficiency.

In this guide, we’ll break down the CIP vs CIL gold recovery processes, explain how each system works, and help you decide which is best for your operation.

What Is Carbon in Pulp (CIP)?

CIP Gold Recovery Process Overview

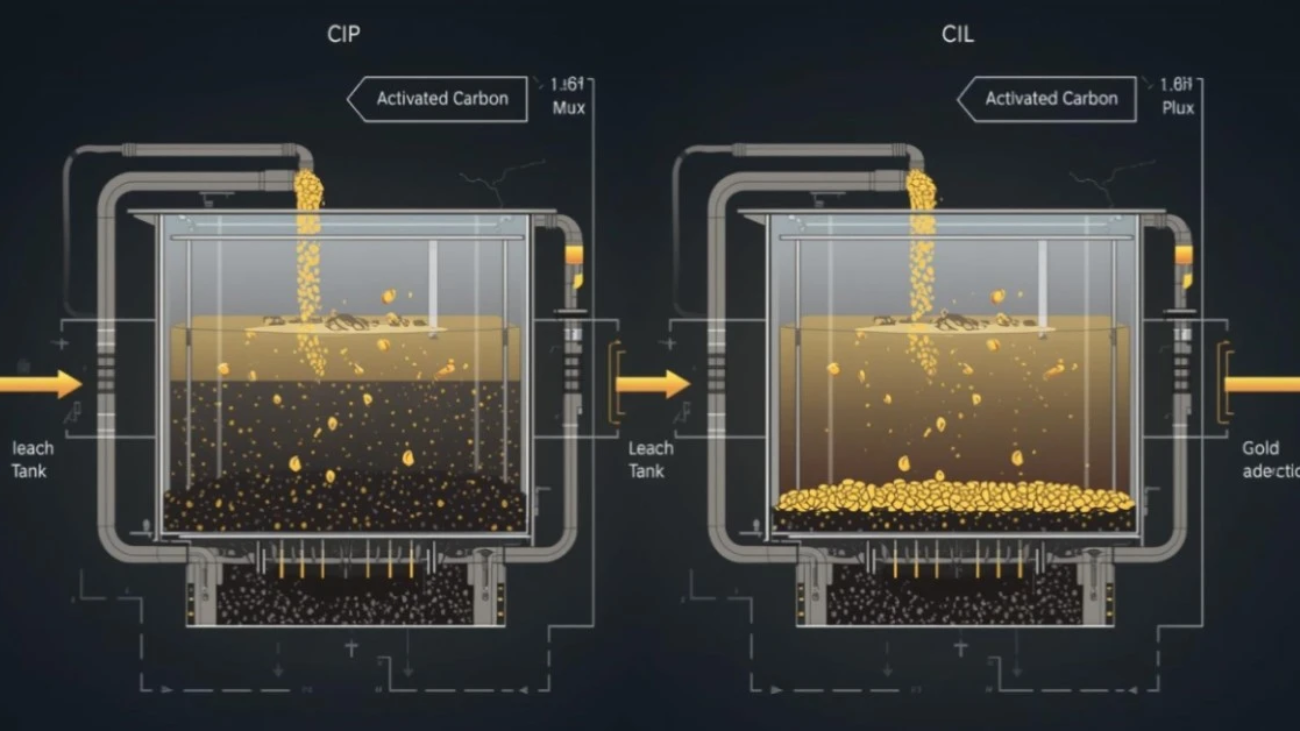
In the Carbon in Pulp (CIP) process, gold is leached from crushed ore using a cyanide solution in large leach tanks. Once the gold is in solution, activated carbon is added to the pulp in a series of tanks after leaching is complete.

How CIP Works:

  1. Ore is crushed and mixed with cyanide to dissolve gold into a slurry.
  2. After leaching, activated carbon is added to adsorb gold from the solution.
  3. The gold loaded carbon is separated and sent for gold recovery.
  4. The slurry is recycled or discarded.

Key Factors in CIP:

  • Carbon particle size and hardness
  • Agitation and tank design
  • Slurry residence time
  • Screen efficiency for carbon separation

What Is Carbon in Leach (CIL)?

CIL Gold Recovery Process Overview

Carbon in Leach (CIL) integrates leaching and adsorption into a single step. Activated carbon is added directly to the leach tanks, allowing gold to be adsorbed as it dissolves.

This approach increases efficiency by reducing gold losses that occur in intermediate transfer steps. CIL is especially advantageous for ores with slow leaching characteristics.

How CIL Works:

  1. Crushed ore is added to leach tanks with cyanide and activated carbon.
  2. Gold dissolves and is immediately adsorbed onto carbon in the same tank.
  3. Carbon is separated, and the gold is recovered from it.

Key Parameters in CIL:

  • Cyanide concentration
  • Dissolved oxygen levels
  • Pulp density
  • Temperature and retention time

Activated Carbon’s Role in Gold Recovery

The efficiency of both CIP and CIL systems is driven by the performance of activated carbon, typically made from coconut shell for its:

  • High mechanical strength
  • Excellent microporous structure
  • Regenerability through thermal reactivation

Why Activated Carbon Works So Well:

  • Surface area > 1000 m²/g
  • High adsorption capacity for gold cyanide complexes
  • Reusability through acid washing and thermal reactivation
  • Improved kinetics due to surface chemistry advancements

Modern carbon formulations enhance throughput and reduce attrition losses, improving overall plant performance.

CIP vs CIL: Key Differences and Comparison

FeatureCIP (Carbon in Pulp)CIL (Carbon in Leach)
Leaching and AdsorptionSeparate stepsCombined in a single tank
Adsorption TimingAfter leaching is completeSimultaneous with leaching
System ComplexitySimpler carbon handlingRequires tighter process control
Gold Recovery RateHigh (up to 95%)High to very high (up to 97%)
Best ForFree milling oresRefractory or slow leaching ores

Advantages of CIP and CIL Gold Recovery Systems

  • High recovery rates (often >95%)
  • Scalable and flexible for various ore types
  • Reduced capital and operating costs
  • Lower environmental impact vs older methods (e.g., Merrill Crowe)
  • Efficient carbon regeneration and reuse
  • learn more about advantages of activated carbon in Gold recovery

Which System Should You Choose?

  • Choose CIP if your ore has fast leaching kinetics and a simpler plant layout is preferred.
  • Choose CIL for complex, refractory, or slow leaching ores where maximizing recovery is critical.

In many modern mining operations, CIL is favored due to its compact design and slightly higher recovery rates—but it does require more precise control.

Conclusion

CIP and CIL are industry leading gold recovery technologies that harness the exceptional adsorption properties of activated carbon to deliver high recovery rates, operational efficiency, and scalability in modern mining operations. Whether you choose Carbon in Pulp or Carbon in Leach, the quality of activated carbon used plays a critical role in the overall success of your gold extraction process.

Ozechem offers premium grade activated carbon specifically engineered for gold recovery applications. With Ozechem’s activated carbon, you can enhance adsorption efficiency, reduce losses, and improve the overall economics of your gold recovery operation.