Activated Alumina Catalyst Support
Activated alumina catalyst support plays a critical role in modern refining, petrochemical processing, gas treatment, and environmental protection systems. As a highly porous and thermally stable material, activated alumina provides the structural and surface foundation required for efficient catalytic reactions across multiple industries.
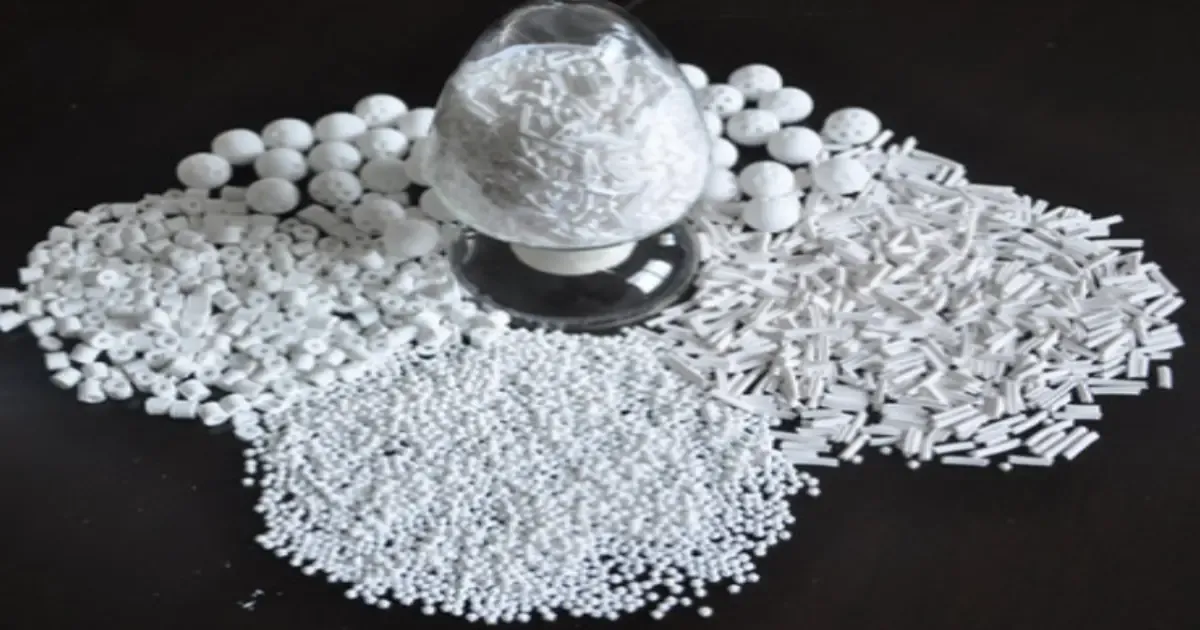
In the Middle East, especially with growing refining and petrochemical capacity, demand for Activated alumina catalyst support in UAE and across GCC countries continues to rise. Industries require reliable alumina catalyst support material that delivers consistent surface performance, high mechanical strength, and stable behavior under extreme operating conditions.
What is Activated Alumina Catalyst Support?
Activated alumina catalyst support is a high surface area aluminum oxide material designed to hold and disperse active catalytic components such as metals or metal oxides. It provides:
- Large internal surface area
- Controlled pore size distribution
- Strong mechanical structure
- Excellent thermal stability
As a porous alumina catalyst support, it enhances catalyst dispersion and ensures optimal reactant contact, improving overall reaction efficiency.
Many industries in the region rely on Activated alumina for catalyst carriers in UAE due to its reliability in high demand refining and gas processing environments.
How Activated Alumina Works as a Catalyst Support?
Understanding how activated alumina works as a catalyst support helps in selecting the right material for industrial reactors.
Activated alumina does not typically act as the active catalyst itself. Instead, it functions as a structured carrier that:
- Provides catalyst support active sites
- Enhances alumina support interaction with catalysts
- Controls mass transfer through its pore network
- Improves adsorption performance of activated alumina catalysts
The surface chemistry of alumina catalyst support allows strong anchoring of catalytic metals, preventing sintering and improving catalyst life. In many industrial systems, activated alumina support for catalytic reactions ensures stable and repeatable performance under harsh conditions.
Structural Properties and Surface Characteristics
High Surface Area and Pore Structure
A key feature of high surface area alumina catalyst support is its optimized internal structure. The alumina support material surface area directly affects dispersion of active components and reaction efficiency.
The activated alumina pore structure for catalysts is engineered to:
- Facilitate diffusion of reactants
- Enhance contact time
- Improve catalyst support adsorption characteristics
As a porous alumina catalyst carrier, the material balances micro and mesopores to ensure optimal catalytic performance.
Mechanical and Thermal Strength
Industrial reactors operate at elevated temperatures and pressures. Therefore, alumina catalyst support mechanical strength is essential.
A durable activated alumina catalyst support provides:
- High crushing strength
- Stable shape retention
- Resistance to attrition
Its alumina catalyst support thermal properties make it suitable for high temperature catalyst support media used in refining and petrochemical units.
Applications in Refining and Petrochemicals
Hydrocarbon Conversion and Refining
In refinery environments, activated alumina for hydrocarbon conversion catalysts is widely used. It supports catalysts in cracking, reforming, and hydrogenation processes.
Industries seeking the best activated alumina catalyst support for refining prioritize materials with optimized pore distribution and structural stability.
Applications include:
- Alumina catalyst carrier for refining
- Catalyst carrier for hydrocarbon conversion
- Catalyst support media for oil refining units
In the region, activated alumina for petrochemical catalysts in UAE supports large scale refining and petrochemical production.
Hydrogenation and Gas Phase Reactions
Activated alumina is frequently used in activated alumina in hydrogenation catalysts due to its stability and surface compatibility.
As a catalyst carrier for gas phase reactions, it provides:
- Uniform dispersion of active metals
- Controlled mass transfer
- Enhanced catalyst longevity
These features make it ideal for activated alumina catalyst carriers for hydrogen production and other gas phase chemical processes.
Oxidation and Environmental Catalysis
In emission control and environmental treatment systems, alumina support in oxidation reactions plays an important role.
- Catalyst support in oxidation processes
- Alumina support for environmental catalysts
- Activated alumina for environmental catalysis
- Alumina catalysts for gas cleaning
These systems are increasingly used in the UAE and GCC to meet stricter environmental regulations.
Industrial Uses Across the Oil & Gas Sector
Activated alumina is essential as catalyst support for oil & gas processing. Its stability under fluctuating pressure and temperature conditions makes it ideal for:
- Gas purification
- Reforming reactors
- Petrochemical feedstock upgrading
Companies searching for petrochemical catalyst support solutions require consistent material performance and long service life.
As a high performance alumina support for the petrochemical industry, activated alumina ensures high conversion efficiency and reduced catalyst deactivation.
Selecting the Right Catalyst Support
When selecting alumina catalyst support media, key factors include:
- Surface area requirements
- Pore volume and distribution
- Mechanical strength
- Thermal resistance
Proper catalyst support design with activated alumina ensures compatibility with specific catalytic metals and reaction conditions.
Understanding catalyst support media surface area effects helps optimize reactor productivity.
Buy OOZECHEM premium Activated Alumina For Catalyst
Catalyst Support Materials Comparison
In an industrial catalyst support materials comparison, activated alumina stands out due to:
- High surface area
- Strong mechanical durability
- Excellent thermal stability
- Reliable adsorption characteristics
Compared with other oxide supports, it offers better catalyst support stability and durability in demanding oil and gas operations.
Regional Supply and Market Presence
The demand for Activated alumina catalyst support in UAE continues to grow with expanding refining capacity. Companies often look for:
- Catalyst support media supplier in KSA
- Alumina catalyst carrier for GCC industries
- Industrial catalyst support solutions in Middle East
- Activated alumina catalyst support exporter
Reliable supply ensures uninterrupted operations for refineries, chemical plants, and gas processing facilities.
Performance in Chemical Reactors
As alumina support for chemical reactors, activated alumina enables:
- Uniform catalyst distribution
- Stable long term operation
- Reduced pressure drop
Its use in catalyst support media for chemical processing ensures consistent reaction performance across multiple industrial applications.
Conclusion
Activated alumina remains one of the most trusted and widely used materials in catalytic engineering. From catalyst support solutions for oil & gas to environmental oxidation systems, it delivers reliable structural and surface performance.
With its optimized pore structure, mechanical integrity, and adaptable surface chemistry, activated alumina ensures efficient catalytic reactions across multiple industrial sectors. As demand for advanced refining and petrochemical operations grows in the Middle East, high quality activated alumina support media continues to be a critical component of modern catalytic systems.
Also Check Other Applications:
More Activated Alumina guides
Tell us the duty. We will quote the grade.
Send the product, the volume and the destination port. We come back with grade, packing and delivered price within one business day.